Category: Solvent Recyclers

How Automated Solvent Recycling Supports Smarter, More Connected Manufacturing 
27Feb

How Automated Solvent Recycling Supports Smarter, More Connected Manufacturing 

Introduction: Automation Beyond the Production Line As manufacturers continue to invest in automation, digitalization, and connected systems, one area is often overlooked: solvent recovery. Traditionally treated as a standalone utility, solvent recycling plays a critical role in safety, efficiency, and operational consistency especially in Class 1 Division 1 (C1D1) environments. Modern automated solvent recycling systems, […]

Solvent Recycling for High-Boiling Solvents: Challenges and Solutions 
16Feb

Solvent Recycling for High-Boiling Solvents: Challenges and Solutions 

High-boiling-point solvents play a critical role in many industrial processes—from inks and coatings to oils, greases, adhesives, and specialty chemical formulations. They are also among the most challenging materials to recover efficiently. Facilities often discover that standard solvent recycling approaches that work well for low- or mid-boiling solvents struggle when boiling points rise, contamination increases, […]

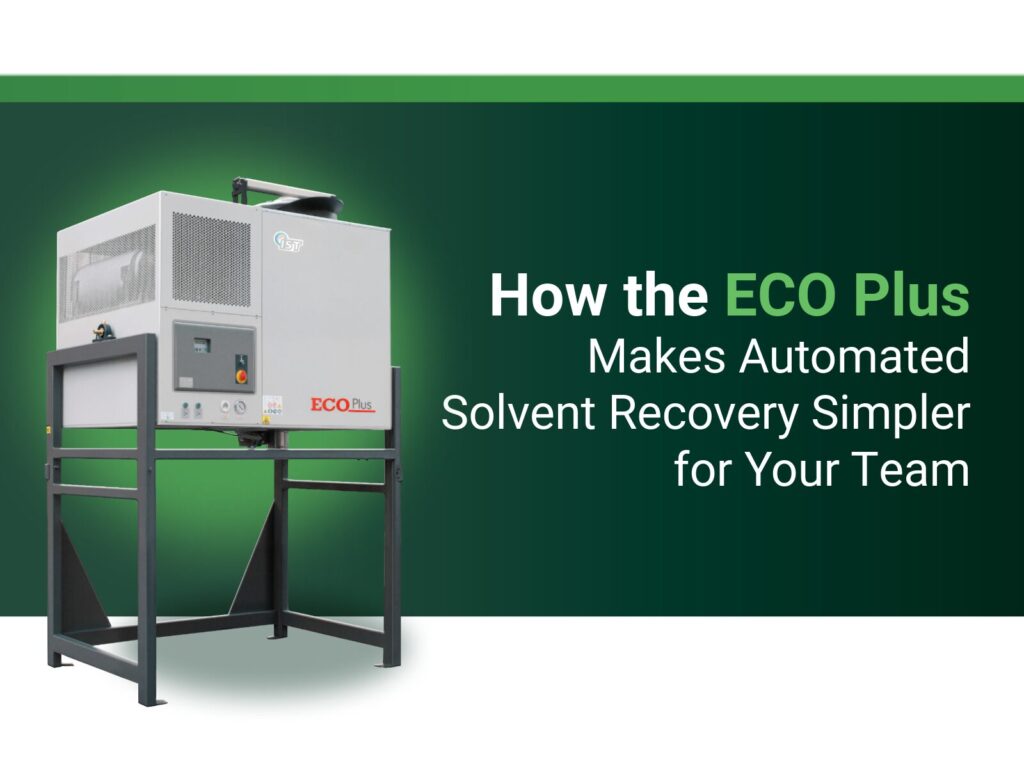
How the ECO Plus Makes Solvent Recovery Simpler for Your Team
10Feb

How the ECO Plus Makes Solvent Recovery Simpler for Your Team

The ECO PLUS distillers are expandable systems designed for intelligent integration in existing facilities. Conceived for continuous operation, ECO PLUS distillers can recover up to 528 gallons of contaminated solvent a day. Their numerous optional accessories, ease of integration with existing production lines, and high level of automation have made these distillers a success in […]

Subscribe and get the latest news
Download the ECO Plus brochure